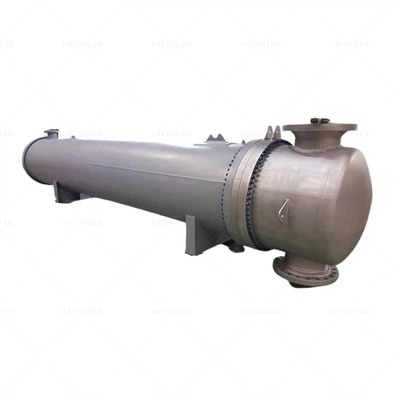
If you’ve ever driven past a refinery, a chemical plant, or even a power generation facility that runs on natural gas, there’s a good chance you’ve walked past a shell and tube heat exchanger—big, clunky, silvery units that hum quietly as they move heat from one process stream to another. As a shell heat exchanger supplier, I get asked all the time how these things actually come to life. It’s not just slapping together pipes and a big outer shell, like some new engineers assume. There’s a precise, step-by-step design process that balances scientific accuracy, safety standards, and the specific needs of each customer. Over the 12 years I’ve worked in this field, I’ve seen how cutting corners during design leads to downtime, lost revenue, and even safety hazards, so I’m big on walking through every step like it’s a conversation, not a textbook. Shell Heat Exchanger

It all starts with the customer’s problem. A few months back, we got a call from a mid-sized ethanol plant in the Midwest. Their old exchanger kept overheating, causing fermentation batches to be discarded, and their maintenance team was spending 10 hours a week cleaning fouled tubes. They didn’t need a one-size-fits-all unit—they needed something that would handle their 85°C ethanol stream efficiently, resist fouling from yeast sediment, and fit into a tight space between their distillation column and storage tank. That’s the first step for every project: discovery. We don’t just ask what size they want. We ask what two fluids they’re exchanging heat, what their flow rates are, the temperature they need each stream to reach, any corrosive or abrasive properties of the fluids, how much pressure the unit will operate under, and even if there’s a space constraint from their existing piping. I always tell our sales team that this is the most important part of the whole process—if you get this wrong, nothing else matters. Once we had all those details from the ethanol plant, our design team moved on to the next step: thermal and hydraulic modeling.
This isn’t using a cheap calculator or a basic spreadsheet. We use industry-recognized software—HTRI (Heat Transfer Research Inc.) is the gold standard here, and we also leverage our own in-house formulas that we’ve refined over hundreds of projects. The goal here is to figure out exactly how much heat we need to transfer, and how to get that transfer done without wasting energy or causing damage. For the ethanol plant, our thermal model told us we needed a heat duty of 1.2 MW—enough to raise 200,000 pounds of water per hour from 25°C to 75°C using the hot ethanol stream, which would drop from 85°C to 35°C in the process. Next, we looked at hydraulics: how fast the fluids will flow through the shell and tubes, to avoid pressure drops that would require the plant to spend extra energy on pumps, but also to make sure the flow isn’t so slow that sediment settles. We also calculated fouling factors—numbers that account for the gunk that builds up on tube walls over time, which reduces heat transfer. For the ethanol plant’s yeast, we used a fouling factor of 0.0002 m²·K/W, which is specific to biological fouling, not the higher numbers we’d use for oil or crude sediment. This step can take a week or two, depending on how complex the application is. If a customer has a supercritical CO2 stream in a carbon capture plant, that’s way more complex than basic water and ethanol, so modeling takes longer.
Once we have the thermal and hydraulic data, we move to geometry design. This is where we pick the physical parts that will hold all that heat transfer. The core of a shell and tube exchanger is the tube bundle—hundreds of thin metal tubes, held in place by tube sheets at each end, and supported by baffles inside the shell. Baffles are the metal plates that force the shell-side fluid to zig-zag across the tubes, instead of flowing straight through, which increases heat transfer. For the ethanol plant, we decided on a 16-inch diameter shell, with 316L stainless steel tubes (to resist corrosion from ethanol and yeast), 12 feet long, arranged in a triangular pitch (the standard for higher heat transfer, since it packs more tubes into the same space). We chose segmental baffles with a 25% cut—meaning the baffle leaves 25% open area at the bottom and top of the shell—to balance flow efficiency and pressure drop. We also sized the inlet and outlet nozzles to match the customer’s existing piping, so they wouldn’t have to modify their plant to fit the new exchanger. A lot of new designers will pick a random baffle cut, but we always test different cuts in the model to find the sweet spot. Too small a cut and you get too much pressure drop, making pumps work harder. Too large and the flow doesn’t zig-zag enough, so heat transfer is weak.
Next up is mechanical design and compliance. This is where we make sure the unit is safe, can handle the pressures and temperatures it will see, and meets all global standards like ASME Boiler and Pressure Vessel Code Section VIII, which is non-negotiable in the U.S., and PED (Pressure Equipment Directive) for our European customers. The shell, tube sheets, and channel ends all have to be designed to withstand the maximum operating pressure, plus a 10% safety factor as required by code. For the ethanol plant, their unit operates at 150 psig on the shell side (the cold water) and 50 psig on the tube side (the hot ethanol), so we sized the shell wall to 0.375 inches thick, and the tube sheets to 1.5 inches thick. We also designed the header boxes (the channels at each end of the unit where the fluid enters and distributes across the tubes) to have smooth transitions, to prevent turbulence that would wear on the tubes or cause pressure loss. We also had to consider maintenance here: the ethanol plant wanted to be able to clean the tubes in place if possible, so we designed the channel ends to be removable, so they can pull the tube bundle out without cutting or welding. That’s a big plus for our customers—every design we do has to account for how easy the unit is to maintain, because downtime costs them money. A few years back, a refinery customer told us they’d rather pay a little more for a unit that’s easy to clean than a cheaper one that takes three days to disassemble. That stuck with me.
After mechanical design comes stress analysis. Even if all the dimensions meet code, metal expands when heated, and that can cause stress on the tubes and shell if they’re different materials or operating at different temperatures. This is where expansion joints or U-tubes come in. For the ethanol plant, the shell is at a lower temperature than the tubes (the water is cold, the ethanol is hot), so we used a fixed tube sheet design with an expansion bell on the shell to absorb the difference in thermal expansion. If we didn’t add that bell, the stress would crack the tube sheets within a few months of operation, leading to leaks. We ran finite element analysis (FEA) simulations to test the stress distribution across the entire unit, looking for weak points—areas where the metal might bend or crack under pressure, temperature changes, or even the weight of the unit itself. This step is critical for units operating at high temperatures, like in steam boilers or gas processing plants, where thermal expansion differences are extreme. I remember a project a few years ago for a power plant that operated at 500°C—if we’d skipped the FEA, the unit would have failed within a week.
Once all the design checks are done, we move to prototype testing if needed, though most standard units don’t need a full prototype—our modeling software is accurate enough that we only test custom, high-risk units. For the ethanol plant, which was a custom project, we did a shop test at our facility before shipping. We connected the unit to test lines that mimic their actual process conditions, ran hot fluid through the shell and cold through the tubes, and measured the heat transfer rate, pressure drop, and any leaks. We found a small issue during the test: the baffle spacing was a little too wide, which reduced heat transfer by 8% from what the model predicted. We adjusted the spacing by 2 inches, reran the test, and hit the exact target. That’s why testing is non-negotiable for custom projects—no model is perfect, and catching small issues in the shop is way cheaper than fixing them at the customer’s plant after installation.
The final step is documentation and delivery. We send the customer full as-built drawings, material test reports, compliance certificates, maintenance instructions, and a 1-year warranty on all parts and workmanship. For the ethanol plant, we also included a spare tube bundle and a guide for their maintenance team on how to pull and clean the bundle without damaging it. We ship the units fully assembled, pressure-tested, and tagged with all the relevant codes, so the customer can install it without delays.
At the end of the day, designing a shell heat exchanger isn’t just about numbers and software. It’s about solving a real problem for a real customer, whether that’s keeping an ethanol plant from wasting batches, helping a refinery meet emissions standards, or allowing a power plant to run more efficiently. Every step we take—from the initial discovery call to the final test—is focused on making sure the unit works for them, not just checks our boxes. If you’re in the market for a shell heat exchanger and want a design that’s tailored to your needs, feel free to reach out to discuss your project and get a tailored quote.
Sullair-IHI Compressor Cooler References
- Heat Transfer Research Inc. HTRI Standard for Thermal and Hydraulic Design of Shell and Tube Heat Exchangers
- American Society of Mechanical Engineers. ASME Boiler and Pressure Vessel Code, Section VIII: Pressure Vessels
- Kern, D. Q. Process Heat Transfer. McGraw-Hill, 1950
- European Committee for Standardization. Pressure Equipment Directive (PED) 2014/68/EU
Changzhou Vrcooler Refrigeration Co., Ltd.
Changzhou Vrcooler Refrigeration Co., Ltd. is one of the most professional shell heat exchanger manufacturers and suppliers in China, specialized in providing high quality aftermarket service. Please rest assured to buy high-grade shell heat exchanger for sale here from our factory. For price consultation, contact us.
Address: No. 18-69,Changwu Zhong Road, Wujin district, Changzhou, Jiangsu
E-mail: info@vrcooler.com
WebSite: https://www.vrcooler.com/
